Novelis Aluminium Rolling Mill Output: Standards, Alloys, and Acceptance
-
The Novelis Aluminium Rolling Mill: Production Context
-
Which Standards Govern Aluminium Rolling Mill Output?
-
How Do Alloy and Temper Selection Shape Mill Products?
-
Market and Supply-Chain Signals Reaching Novelis' Mills
-
How Does In-Plant Handling Affect Coil Quality?
-
Technological Updates in Rolling Mill Capability
-
How Should Engineers Respond to the Standards Update Landscape?
An engineer specifying aluminium from a Novelis rolling mill cannot treat a mill reference as a uniform commodity. The output is defined by an evolving pair of standards—ASTM B209/B209M-21a and the EN 485 family—and by market disruptions such as the downtime at Novelis' Oswego mill in New York, which Alcoa's 2025 results directly tie to automotive slab demand. The practical path from alloy and temper selection to final acceptance runs through ordering clauses, tolerances, inspection, and documentation; missing that path returns rejected coils and failed audits.
The Novelis Aluminium Rolling Mill: Production Context
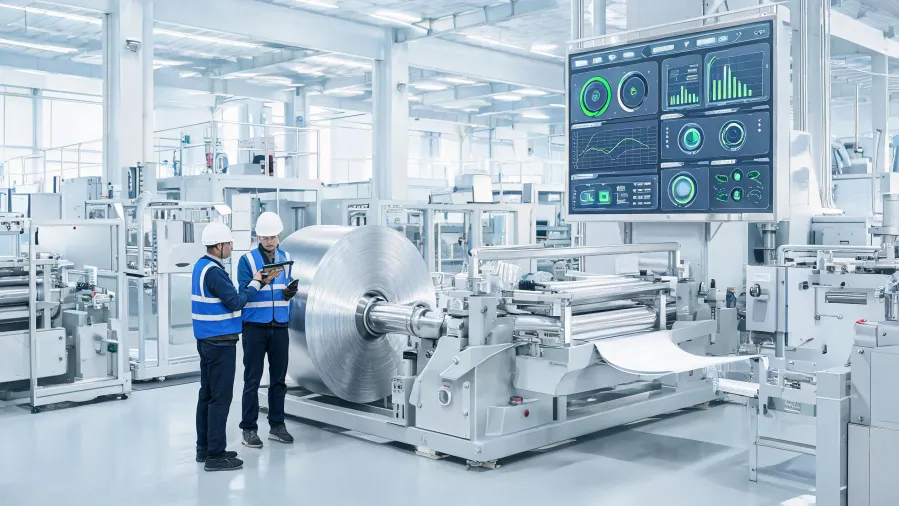
The Novelis group operates a network of aluminium rolling mills that convert cast slab into coil, sheet, and plate for packaging, automotive, and industrial markets. In the global flat-rolled market, these mills occupy a central position: the global aluminium coil and sheet market, estimated at about USD 120 billion in 2025, is projected to reach USD 180 billion by 2034, a compound annual growth rate of 5.1 percent. Novelis is consistently listed among the key players in that market, alongside Hindalco, Constellium, UACJ, and Arconic. The mill itself is where alloy chemistry, rolling practice, and surface finish come together; the output is not a generic ingot but an engineered product with specified thickness, temper, and finish. At the most basic level, a rolling mill takes a hot or cold slab and reduces it through successive rolls until the required gauge is reached. For Novelis, that process is strategic: the company's sheet and coil feed beverage can stock, automotive body panels, and architectural products.
Commercial weight follows from that reach. A procurement intelligence report notes that Novelis' annual revenue exceeds USD 17.5 billion, major mill lead times typically run 16 to 24 weeks, and brand premiums range from 20 to 35 percent. Those figures frame delivery risk and cost for an engineer. The same report also ties Alcoa's 2025 full-year results to a concrete example: downtime at Novelis' Oswego mill in New York softened automotive slab demand, showing how one mill's operational state can shift national supply-demand balances. Novelis is thus not a faceless commodity producer; it is a supply-chain node whose performance directly affects material availability and price. Engineers who track market data can anticipate when to expedite orders or qualify alternative suppliers, using signals such as the Oswego disruption to time procurement.
Which Standards Govern Aluminium Rolling Mill Output?
The output of such a mill is defined by formal standards. The most widely cited North American document is ASTM B209/B209M, the Standard Specification for Aluminum and Aluminum-Alloy Sheet and Plate, current as of revision 21a, updated January 12, 2022. It covers flat sheet, coiled sheet, and plate in specified alloys and tempers, with mill finish for heat-treatable alloys and various bright finish options for non-heat-treatable alloys. Importantly, the standard places responsibility for all inspection and test requirements on the producer unless the contract states otherwise. That means the purchaser's order clause determines whether additional verification is needed; otherwise, the mill's own inspection is the acceptance gate. The standard also demands that material be commercially sound and uniform, with identification marking and conformance to general quality requirements. For a Novelis order, a buyer who invokes B209/B209M-21a without specifying extra inspection tests is deferring to the mill's quality system, which is precisely why the standard revision and order clauses matter.
Across the Atlantic, the ordering workflow is different. The GDA/EAA guide, How to Order Aluminium Products According to EN Standards, third edition, November 2008, sets out the system: flat rolled products are ordered according to EN 485-1, which defines tolerances and technical conditions. The guide was revised by, among others, Peter Furrer of Novelis AG, a sign of how closely the producer community shapes the standard. A critical consequence emerges: ordering to EN 485 imposes different ordering clauses, tolerances, and documentation than ordering to ASTM B209. Engineers who assume the standards are interchangeable can find coils rejected at incoming inspection or at the end-user's audit. The timeline is telling: the Aluminum Association's in-plant handling guide reached its second edition in January 2006, the EN 485 ordering guide its third in November 2008, and ASTM B209 was last updated in January 2022, so documents are not static. An engineer must verify which version of the standard the mill is operating to, and what the order actually says.
How Do Alloy and Temper Selection Shape Mill Products?
The choice between 7075 and 6061 illustrates why alloy and temper matter more than the mill reference. 7075, in the 7xxx series, uses zinc and copper as primary alloying elements, with a typical composition of 5.6% zinc and 1.6% copper. 6061, in the 6xxx series, relies on silicon and magnesium, around 0.6% silicon and 0.1% magnesium. In the T6 temper, 7075 has a tensile strength nearly double that of 6061, making it a common aerospace alloy. 6061, by contrast, offers better corrosion resistance, weldability, and formability, and is typical in structural, marine, and automotive applications. The composition also drives cost and supply: 7075 is generally more expensive and less corrosion resistant when unprotected. For a mill order, the difference is not a minor tweak; it changes mechanical behavior, corrosion performance, joining requirements, and the temper designation matters as much as the alloy number.
The temper system itself is a specification language. Non-heat-treatable alloys achieve strength by cold working and are designated with H, such as H14 (work hardened) or H24 (partially annealed). Heat-treatable alloys use T, with natural ageing designated T1–T4 and artificial ageing T5, T6, T9. Artificial ageing, for example, requires holding at 100–200 °C for 2–30 hours, and the resulting strength increment is greater than with natural ageing. When an engineer writes 6061-T6 or 7075-T6 on an order, they are not naming a generic grade but a specific processing path. Ordering the wrong temper can leave a part under-stressed or over-brittle, which is why ASTM B209 and EN 485 both require the temper designation to be explicitly stated. In practice, a mill will roll to the specified temper only if the order lists it correctly; a vague reference to 'temper T' or 'H temper' invites interpretation and increases the risk of non-conforming material.
Market and Supply-Chain Signals Reaching Novelis' Mills
Consider the evidence from early 2026. Alcoa, reporting full-year 2025 results, flagged that automotive slab demand continues to face headwinds stemming from the impacts of downtime at Novelis' Oswego mill in New York, which has weighed on automotive-related flat-rolled demand dynamics. This is a concrete, dated signal: a single mill outage in upstate New York could shift regional supply-demand balances for automotive sheet. For a procurement engineer, such market news is not background noise; it changes lead-time expectations and may justify dual sourcing or inventory buffers. The same report noted that China is nearing its smelter capacity cap, so supply growth will concentrate outside China, keeping disruption risk elevated. These signals also influence contract terms: when a major mill slows, buyers often push for force majeure clauses or longer acceptance windows. The Oswego example, in particular, shows that mill-level disruptions are not merely hypothetical; they show up in a primary producer's earnings statement.
The broader market context reinforces this. The global aluminium coil and sheet market was estimated at USD 120 billion in 2025, with a projected USD 180 billion valuation by 2034 and a CAGR of 5.1% (by one report) or 5.2% (by a parallel report). Packaging, transportation, and construction are the primary applications, and the alloy families are spread across the 1xxx, 2xxx, 3xxx, 5xxx, 6xxx, and 7xxx series. The two reports name Novelis among the key players, confirming its systemic role. The growth, however, is not evenly distributed: automotive sheet demand is sensitive to mill-level disruptions, while packaging demand is steady. An engineer evaluating aluminium supply should therefore distinguish the segments; a robust packaging market cannot offset a weak automotive sheet line. Moreover, the presence of regional capacity constraints, such as China nearing its smelter cap, means that mill-level events can propagate into price volatility. In such an environment, a buyer's risk model must include both standard-compliance risk and supply-chain risk.
How Does In-Plant Handling Affect Coil Quality?
Once the coil leaves the rolling mill, in-plant handling becomes a quality determinant. The Aluminum Association's 'Guidelines for In-Plant Handling of Aluminum Plate, Flat Sheet, and Coil' (second edition, January 2006) is the reference for preventing surface damage, staining, and edge damage. The guidelines are voluntary, but they codify industry practice: proper lifting, storage, and separation prevent the finish defects that lead to rejected coils. Because the guide was published in 2006 and the standards have since been updated, an engineer should confirm the mill's current handling procedures match the latest edition; a mill that still uses outdated practices is a risk factor. Staining, in particular, is often traced to moisture or contaminated rolling oil, so handling is inseparable from fluids management.
That link shows up in a case at Alcoa-Köfém's flat-rolled plant in Hungary. The mill set out to reduce rolling oil costs and eliminate staining-related coil rejects. By reprocessing rolling oil—rather than replacing and disposing of it—the plant cut total oil expenses by 60% and eliminated stain-related rejects. The case shows that surface quality is not only a chemistry issue but a fluids-management issue; the quality of filtered oil returned to the process directly affected the finished coil. For an engineer auditing a mill, questions about rolling oil filtration and reprocessing are as relevant as questions about alloy chemistry. The evidence also demonstrates a mechanism: when rolling oil is filtered and reused, the cost per coil falls and the reject rate drops, which is a concrete, auditable improvement.
Technological Updates in Rolling Mill Capability
Technology is reshaping what a rolling mill can deliver. AI-based mill controls, such as those in Alcoa's Micromill technology, now achieve thickness precision beyond conventional gauging systems. In parallel, the Aluminum Association has reorganized its design manual to mirror steel code structures, and new tempers and alloys are documented as they are introduced. This matters for the specifier: a mill updated with AI controls can hold tighter tolerances, which in turn may allow the purchaser to relax downstream machining allowances or reduce scrap. The standards, however, still define the acceptance criteria; a modern mill can exceed tolerance but the inspection clause in the order determines whether the tighter result is certified. In addition, advanced joining technologies, such as friction-stir welding, create demand for plates with stable metallurgical properties, and rolling mills respond by tightening thermal-mechanical control.
A concrete demonstration came on March 30 at NASA's Marshall Space Flight Center, where an 18-foot friction-stir welded and spun-formed tank dome debuted, developed with Alcoa's aluminum-lithium plate and materials expertise. The project, involving Lockheed Martin and MT Aerospace, proved that friction-stir welding can reliably and cost-effectively join large aluminum-lithium plates for high-strength applications. For an engineer, this is not an isolated aerospace story; it signals that large-format, weld-ready plate is becoming a practical option. Rolling mills, including Novelis, are expected to supply material with the flatness and consistency that friction-stir welding requires. The acceptance of such plate still depends on alloy, temper, and flaw acceptance criteria set in the purchase order, not just on the novelty of the joining process.
How Should Engineers Respond to the Standards Update Landscape?
Given this landscape, the engineer's first duty is to verify the governing standard edition. For North American orders, confirm the order references ASTM B209/B209M-21a, not an outdated revision; for European orders, confirm the EN 485-1 ordering rules and the documentation set. The producer is responsible for inspection only when the contract is silent, so a purchaser who wants independent verification must state it explicitly in the order. The non-obvious update is not a new alloy but the workflow: ordering to the wrong standard, or the wrong revision, is the fastest route to rejected coils. A second inspection point is the temper and surface finish specified; both standards define those in detail, and a mismatch between the mill's certificate and the order is a common cause of audit failures.
Second, choose alloy and temper by the application's critical attributes. For high strength and limited corrosion exposure, 7075-T6 may be justified; for weldability, formability, and corrosion resistance, 6061-T6 or -T4 typically wins. The temper designation should be written in full—T6, H14, H24—because the same alloy in different tempers differs mechanically. The decision rule is: specify the alloy, then the temper, then the standard revision, and then the handling and inspection clauses. If any of those four is left vague, the acceptance criteria become fuzzy, and the mill's definition of 'commercially sound' may not match your quality requirement. A standards-literate, evidence-based approach is therefore not optional; it is the professional minimum for anyone specifying Novelis output. This rule applies whether the order is a single coil or a long-term supply agreement.
Standards update, markets shift, and a single mill can change the balance of supply. The only durable asset in this environment is the engineer's own verification workflow: current editions, explicit ordering clauses, and a clear link between alloy, temper, and acceptance test. That is the verdict that should guide every aluminium purchase order.
Ingrid Solberg
Ingrid Solberg is an independent carbon and structural steel analyst covering steel plate, sheet, coil, pipe, beams, rebar, and galvanized products. She applies ASTM A36/A36M and A6/A6M requirements while comparing grade chemistry, yield strength, tensile strength, elongation, dimensional tolerance, weldability, and surface condition. Her evidence-led guides help engineers, fabricators, and procurement teams select suitable steel forms, define purchase specifications, and evaluate mill or service-center offers.