Novelis Beverage Can Sheet Runs 80% Recycled Content on Today's Lines
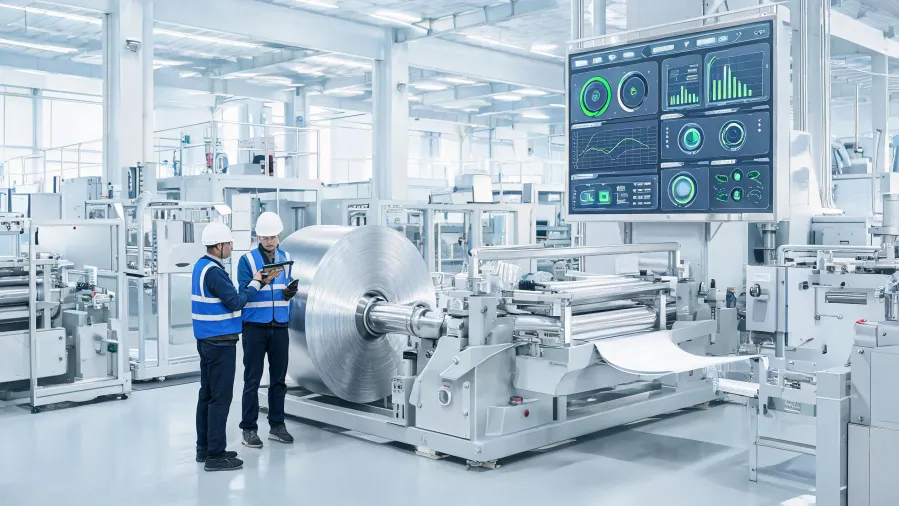
Yes, you can run Novelis beverage can sheet carrying more than 80% recycled content on the presses, trimmers and washers you already have, and the alloy is not what will stop you. The number that decides your trial is your forming and coating window. That window is what the full-scale pilot line in Georgia exists to measure before a commercial coil lands on your uncoiler.
Separate the two decisions and the risk gets small. Recycled content is a feedstock decision, meaning what got melted to make the coil. Gauge, temper and coating are performance decisions about what the metal and the lacquer do at line speed. Novelis sells the first as standard product. You still have to qualify the second on your own tooling.
What Novelis Can Sheet Actually Is
It is aluminum can stock, body sheet and lid sheet, carrying more than 80% recycled content globally and sold as a catalog product rather than a niche grade. Novelis recycles more than 2 million tonnes of aluminum a year, and more than 84 billion used beverage cans move through that loop annually.
The chemistry is familiar. A can body runs on 3104-type alloy with around 1% manganese and 1% magnesium to build strength through the draw; the lid runs on 5182-type, softer, easier to score and open. Recycled content arrives as remelted used-can feedstock blended back to those same registered compositions, then cast, rolled and heat-treated to the temper you order.
So the coil on your uncoiler looks the way it always did: body stock about 0.28 mm thick in H19 temper, lid stock thinner at roughly 0.22 mm. Nothing on the purchase order changed except the origin of the metal.
Recycled Content Is Not a Recyclable Claim
Most people assume a high recycled-content coil is a downgraded metal stream, slightly softer, dirtier and more variable than primary. In fact the alloy specification is identical and the recycled fraction is the same chemistry, because used cans are remelted back to spec instead of being blended into a cheaper one. What changes is where the metal came from, not what it does in the press.
The 80% figure counts recycled input. It says nothing about what happens after the can is collected. A can poured from 100% primary aluminum is still fully recyclable, and a supplier can print that word on packaging made from mined metal. Recycled content and recyclability answer different questions, one about what you buy, one about what happens at the curb.
The loop itself is tight. A used aluminum can is recycled and back on a store shelf in under 60 days, and that cycle repeats without any loss of quality. That is the part that surprises anyone who came up through steel or glass, where recycled feedstock usually does trade off against properties.
So when a supplier's recycled metal drifts off composition, you find out at the trim or the neck, not in a sustainability footnote. Ask for the chemistry certificate on the recycled coil and compare it line by line with the primary one before you buy the campaign.
What Changes on Your Forming and Coating Line
Short answer: your process window moves, not your alloy. Novelis refines formable alloys, coatings and the manufacturing process behind packaging sheet, and the refinements show up as variables you tune at the press, meaning draw and iron loads, necking and beading strains, and the coating cure window.
Start with the draw. Body stock enters around 0.28 mm and the ironing rings pull the wall down to roughly 0.10 mm at mid-body, so a drift in incoming temper or lubricant shows up fast. You see it as earing, the four-lobed rim that has to be trimmed off, or as a flange crack that stops the line.
Coating is the second front. Internal lacquer is baked at roughly 200°C peak metal temperature for a few seconds. Run it cold and adhesion suffers; run it hot and you blister the film. Once the film is gone the beverage chemistry reaches the aluminum, and you get taste and corrosion months later rather than a weight problem on the dock.
Picture the trial: a shop moves a line to recycled-content coil, the first three coils run clean, and a temper shift on coil four starts throwing ears at the trim station. That is scrap at the press that afternoon, and it is the reason a shop lead cares about the window rather than the recycled percentage. Compare the coil with one from a primary-only smelter carrying the same 3104 certificate but a different melt history, and your press will tell you which one holds a wider window.
Barrier Coatings, Wall Thickness, and the Freight Math
Coating and gauge get handled as separate line items. They are not. The internal film is the barrier that keeps beverage chemistry off the aluminum; wall thickness is what holds the can up under axial load. Move one and you have changed the other's job.
Gauge is where the freight money sits. Coils ship by truck, so shaving 0.02 mm off body stock takes about 7% of the shipped metal weight out of the load and raises cans per truck by roughly the same amount. On a high-volume SKU that is real money, which is why lightweighting keeps coming back.
The catch is strength. A can wall resists axial compression roughly with the square of its thickness, so a 7% gauge cut costs about 14% of column strength before anything else changes. Drop under the filler's pallet-load spec and cans crush in the warehouse. Buckle and column strength are the numbers to hold, and both come off an axial compression rig, not an estimate.
Barrier is the other half. A 330 ml carbonated cola and a 500 ml acidic juice do not ask the same thing of the lacquer, so coating spec is set per SKU. A single lacquer chemistry does not fit every fill. Lose adhesion under a thin wall and corrosion pitting and taste carry-over arrive long before the can looks wrong. Barrier, gauge and freight are one linked decision per SKU, not three independent savings.
Why the Pilot Line Sits Ahead of Your Press
At the Global Research and Technology Center in Georgia, customers get cutting-edge labs and a full-scale beverage can pilot line that turns bold ideas into scalable solutions. Full-scale is the load-bearing word: trial cans run at production geometry and speed, through the same stations your plant runs.
Most people assume that pilot line is a marketing tour with a canning demo at the end. In fact it is where recycled-content feedstock and coating changes get qualified against the defects your line will produce, including earing at the trim, adhesion after the bake, and necking strain at the shoulder. If the risk is not burned off there, it is not burned off anywhere.
The sequence is plain. Send your tool geometry, run trial coils, measure earing and wall thickness across the body, pull adhesion after the bake, then commit to commercial tonnage. A lab coupon test on a small blank tells you almost nothing about a full-depth draw at line speed; the pilot line closes that gap.
The doubt that hangs on is that recycled content means variable metal, and that is the one claim a shop can settle with a measurement instead of an argument. If the Georgia trial coils hold earing and adhesion inside your limits, the recycled percentage stops being a process risk and becomes a procurement lever you can carry to the brand owner. If they do not, you paid for a trial instead of a recall.
Ingrid Solberg
Ingrid Solberg is an independent carbon and structural steel analyst covering steel plate, sheet, coil, pipe, beams, rebar, and galvanized products. She applies ASTM A36/A36M and A6/A6M requirements while comparing grade chemistry, yield strength, tensile strength, elongation, dimensional tolerance, weldability, and surface condition. Her evidence-led guides help engineers, fabricators, and procurement teams select suitable steel forms, define purchase specifications, and evaluate mill or service-center offers.